

Klingspor
KLINGSPOR HF 100 F Carbide Burrs
KLINGSPOR HF 100 F Carbide Burrs
GST included. Shipping calculated at checkout.
SKU: 295971
Available to order
Delivery options
Select your suburb for a delivery estimate. Additional courier options are available at checkout.
Estimates are for this item and quantity only, in AUD excluding GST. Final availability, shipping and GST are confirmed at checkout.
Buy with confidence
Delivery & pickupAvailable to order · Lead time varies
Ordered from our supplier. This item is not currently stocked at our store. Contact us to check the expected lead time before ordering. Dispatch depends on supplier availability.
Australia-wide delivery. Available shipping options and costs are shown at checkout.
Free Smithfield pickup. Wait for your Ready for Pickup notification before travelling to the store.
Returns & exchanges90 days for eligible unopened items
Change-of-mind returns are available within 90 days of receiving your order for eligible items. Items must be unused, unopened, complete, in original packaging and resellable condition, with proof of purchase.
You pay return shipping for change-of-mind returns. Original shipping is not refunded. Please request approval before sending an item back.
Exclusions include items marked Special Order, gases and cylinders, hazardous materials, chemicals, and custom or cut-to-length items. See the full policy for all exclusions.
Warranty & supportProduct-specific warranty & support
Manufacturer warranties apply where available. See this product’s specifications or contact our team to confirm the applicable warranty.
For a fault or incorrect item, contact our team with your order details and a description of the issue.
Need help choosing?
Call our Smithfield team for product advice and compatibility checks.
Take a closer look
Product information
Details
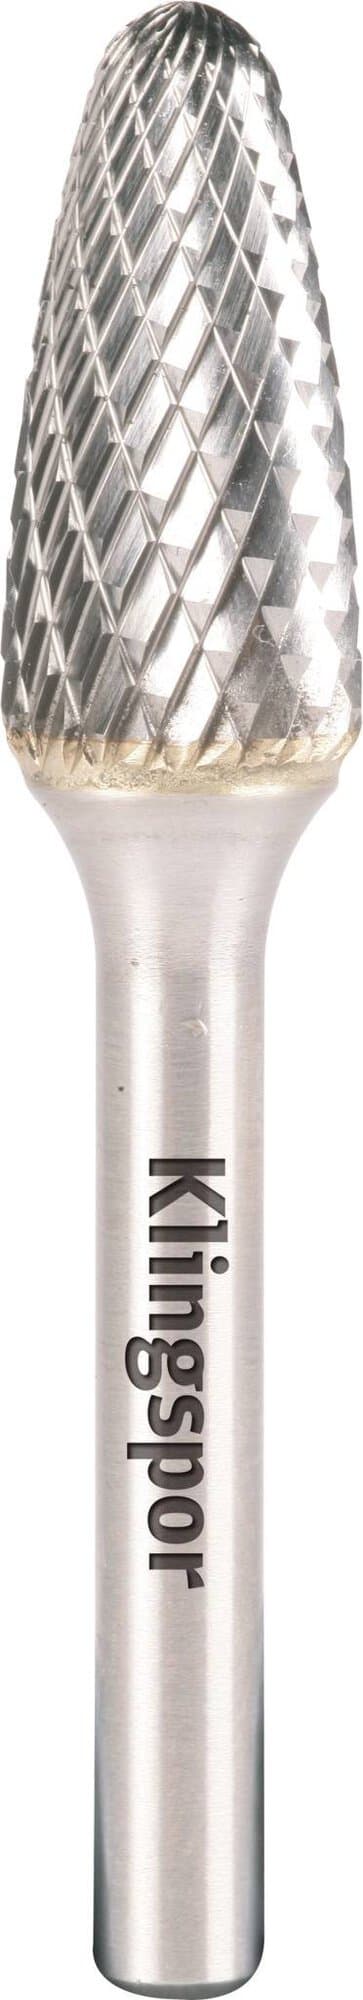
The Klingspor HF 100 F carbide burr has a rounded tree profile for shaping and finishing moulded parts and curved metal surfaces. The rounded cutting end helps the head follow transitions, while the tapered body gives access to areas that a broad cylindrical burr cannot reach as easily.
Sold as a full selling pack: 1 burr. One ordered quantity supplies the complete box, pack or set shown for the chosen SKU.
Features and benefits
- Carbide cutting head for the manufacturer-listed metals.
- Rounded tree profile for contours, cavities and moulded parts.
- Double-cut options support controlled handling and reduced vibration.
- Head diameter, cutting length and shank size are identified for each SKU.
Klingspor specifies this model for construction steel, cast iron, non-ferrous metals and highly heat-resistant materials. Match the head profile and size to the area being shaped, then match the shank to the collet. The appropriate running speed depends on both the head diameter and the workpiece material; choose settings from the manufacturer’s burr guidance instead of treating every size as interchangeable.
Technical specifications
| Brand | Klingspor |
|---|---|
| Form | ball nosed cone |
| Cut | Double-cut (Cut 6) or coarse single cut (Cut 2), as selected |
| Selling quantity | 1 burr |
Variant specifications
| SKU | Dimensions | Configuration | Selling quantity | Diameter | Height | Length | Shank diameter | Shank length | Maximum rotational speed |
|---|---|---|---|---|---|---|---|---|---|
| 295971 | 6 × 18 × 6 mm | Double-Cut; Double-cut | 1 burr | 6 mm | 18 mm | 50 mm | 6 mm | 32 mm | 65,000 rpm |
| 295987 | 9.6 × 19 × 6 mm | Double-Cut; Double-cut | 1 burr | 9.6 mm | 19 mm | 64 mm | 6 mm | 45 mm | 55,000 rpm |
| 296010 | 12.7 × 25 × 6 mm | Double-Cut; Double-cut | 1 burr | 12.7 mm | 25 mm | 70 mm | 6 mm | 45 mm | 35,000 rpm |
| 310277 | 6 × 18 × 6.35 mm | Double-Cut; Double-cut | 1 burr | 6 mm | 18 mm | 51 mm | 6.35 mm | 33 mm | 65,000 rpm |
| 310278 | 8 × 20 × 6.35 mm | Double-Cut; Double-cut | 1 burr | 8 mm | 20 mm | 65 mm | 6.35 mm | 45 mm | 55,000 rpm |
| 310279 | 9.6 × 19 × 6.35 mm | Double-Cut; Double-cut | 1 burr | 9.6 mm | 19 mm | 64 mm | 6.35 mm | 45 mm | 55,000 rpm |
| 310280 | 12.7 × 25 × 6.35 mm | Double-Cut; Double-cut | 1 burr | 12.7 mm | 25 mm | 70 mm | 6.35 mm | 45 mm | 35,000 rpm |
| 296007 | 12.7 × 25 × 6 mm | Coarse Single Cut; Coarse single cut | 1 burr | — | — | — | — | — | — |
| 295985 | 9.6 × 19 × 6 mm | Coarse Single Cut; Coarse single cut | 1 burr | — | — | — | — | — | — |
Selection and use
Choose the burr profile for the surface, cavity, edge or contour being shaped. Match the shank diameter to the machine collet and select the serration for the material and finish required. Cutting-head dimensions and shank diameter are listed separately where available, so the mounting and reach can be checked before ordering.
Maximum RPM and peripheral-speed values are article ratings, rather than recommended working speeds. Use the rating for the selected article and follow the limits marked on the abrasive, mounting accessory and machine.
Product documents
Specifications
The technical details, grouped for easy checking.
No matching specifications. Try another term or clear your search.
Documents & manuals
Keep the setup and technical information close at hand.
Request Pricing or a Quote
Choose the request that suits you and we’ll review the details with this product.