
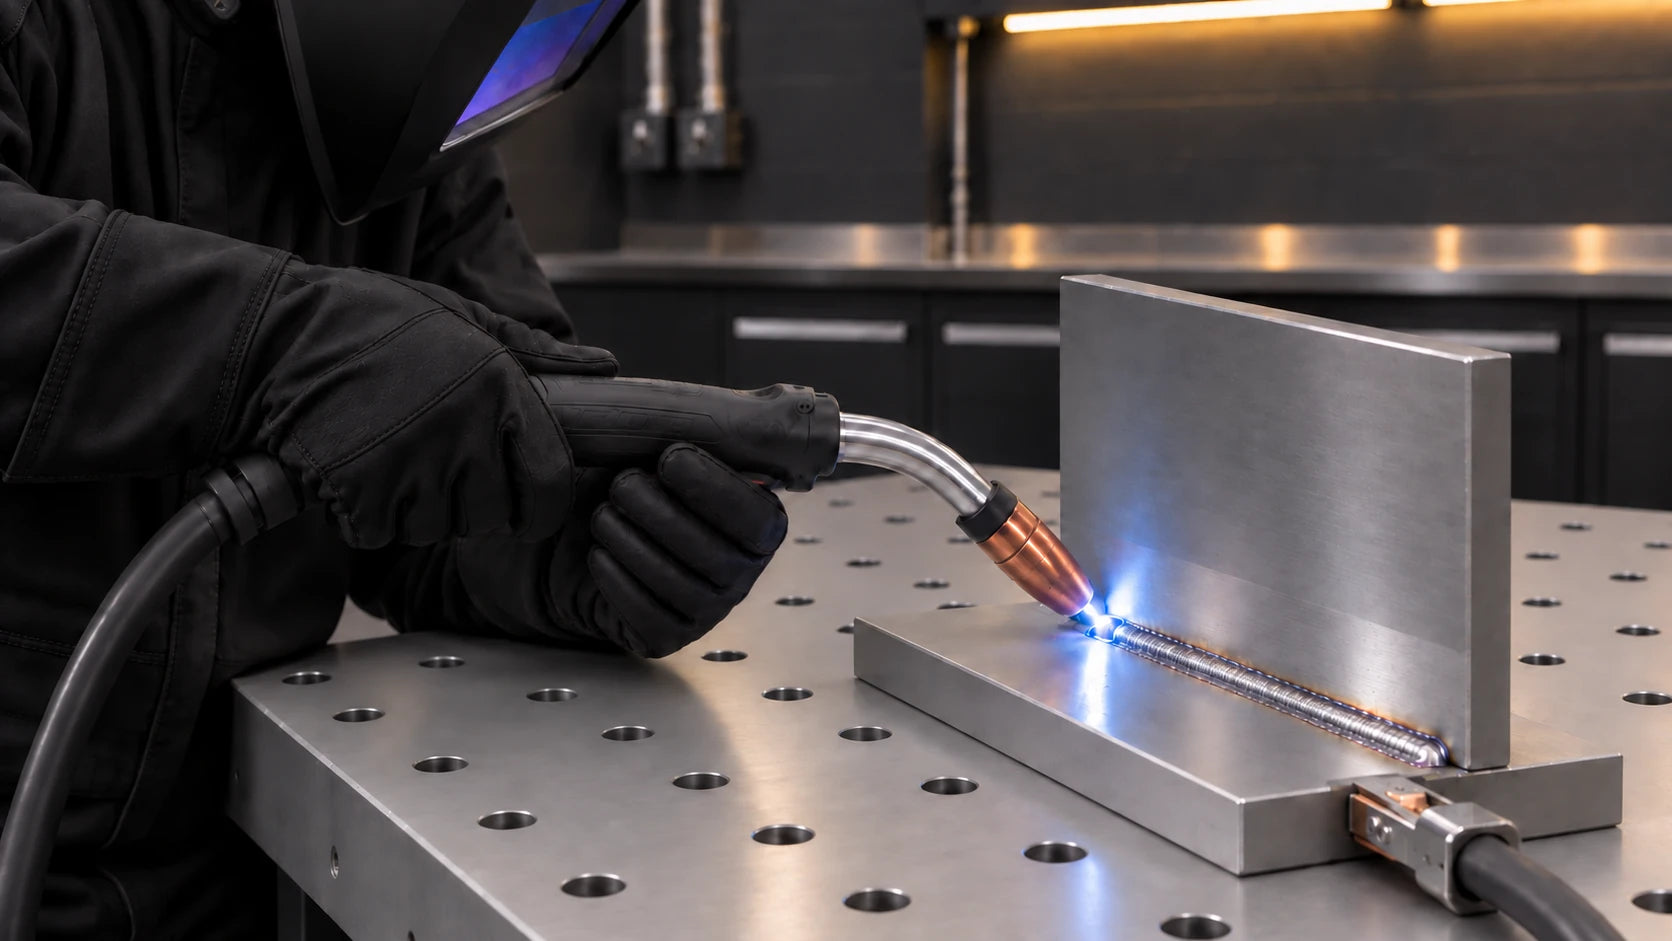
This guide compares common GMAW transfer modes: short circuit, globular, spray and pulsed spray. MIG/MAG terminology depends on the shielding gas; these descriptions are not a claim that droplet transfer occurs only in MIG welding.
Short Circuit
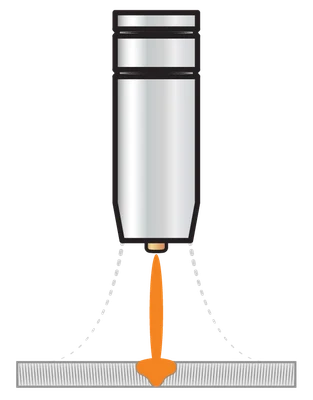
In short-circuit transfer, the wire repeatedly contacts the pool and the short circuit clears. Mild-steel applications commonly use a suitable argon/CO₂ mix or CO₂; other materials need their own gas selection.
Short-circuit transfer is widely used for lower-heat-input work and can suit several positions. Joint suitability and fusion still need to be established by the procedure.
There is no universal 8 mm thickness limit for short-circuit transfer. Joint preparation, root access, passes and procedure qualification determine suitability; lack of fusion is an important risk on heavier sections.
Globular
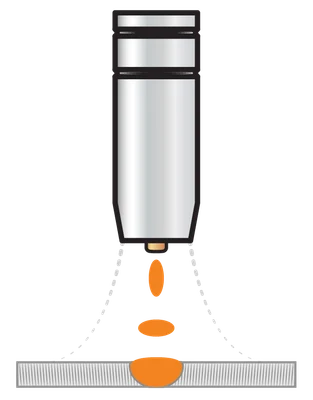
Globular transfer produces relatively large droplets. Gas and settings depend on material and wire; mild-steel examples should not be applied to aluminium or stainless without the appropriate procedure.
The bead appearance isn’t as smooth, and the process itself can be pretty messy with excessive spatter, but it has good penetration.
Globular is hotter in value, with more wire feed speed and voltage than short circuit, so the weld pool is more fluid. Because the pool is more fluid, you’re restricted to flat and horizontal positions only.
Spray
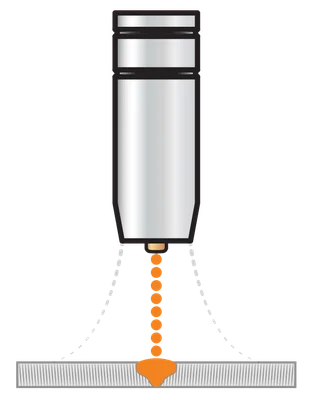
Spray transfer needs a suitable gas and current above the transition for the particular wire. Steel commonly uses an argon-rich mixture; aluminium commonly uses argon. One minimum argon percentage does not cover every material and programme.
It has a much smoother sound than short circuit, with little crackling, almost like a low hissing. The spray method is good for heavy fabrication and thick material as it has a deep penetration profile.
However, it’s so hot and fluid that it’s not suitable for vertical up, vertical down, or overhead welding. It’s a much cleaner process, though, with almost no spatter.
Pulse Spray
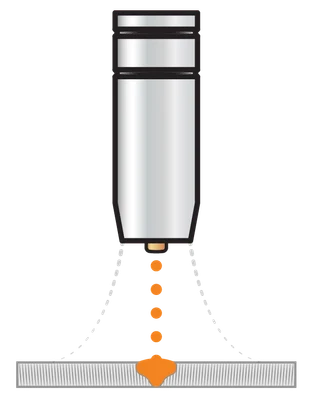
Pulse spray is similar to the standard spray method, but it ‘pulses’ between the set amps (the peak amps) and a low point. Having a low point means that the weld has a moment to cool each time, making the pulse spray transfer more versatile. Because the weld pool has time to (briefly) cool, it isn’t as fluid, so it can be used in more than just flat positions.
Pulsed spray requires a compatible power source and a programme matched to the wire, diameter and gas. Aluminium does not use the same argon/CO₂ mixture as mild steel.
Transfer modes do not form a simple progression of deeper penetration and less spatter. The transition depends on wire, gas and operating conditions; use a supported procedure and verify fusion as well as appearance.
Spray transfer requires the appropriate shielding gas and sufficient current for the wire type and diameter. Raising voltage alone does not establish spray transfer. Select a supported wire, gas and machine programme, then verify the transfer conditions against the welding procedure.
Sources for revised guidance
Reference diagrams: UNIMIG. Original source attribution is retained.
Related guides
Process guideWhat Is MIG Welding? Setup, Wire Feed and Technique TroubleshootingMIG Wire Feeding Problems: A Step-by-Step Troubleshooting Guide Process guideHow to Weld Aluminium: MIG, TIG and TroubleshootingCheck which modes your machine supports.
Have the model, wire, gas and intended application ready.
Ask us about thisTechnical sources and scope
Reviewed 22 September 2026. Manufacturer examples apply to the named equipment; use the current manual for your exact model and the required welding procedure.
Fixed thickness and gas thresholds were removed where they did not apply across materials and programmes.


