
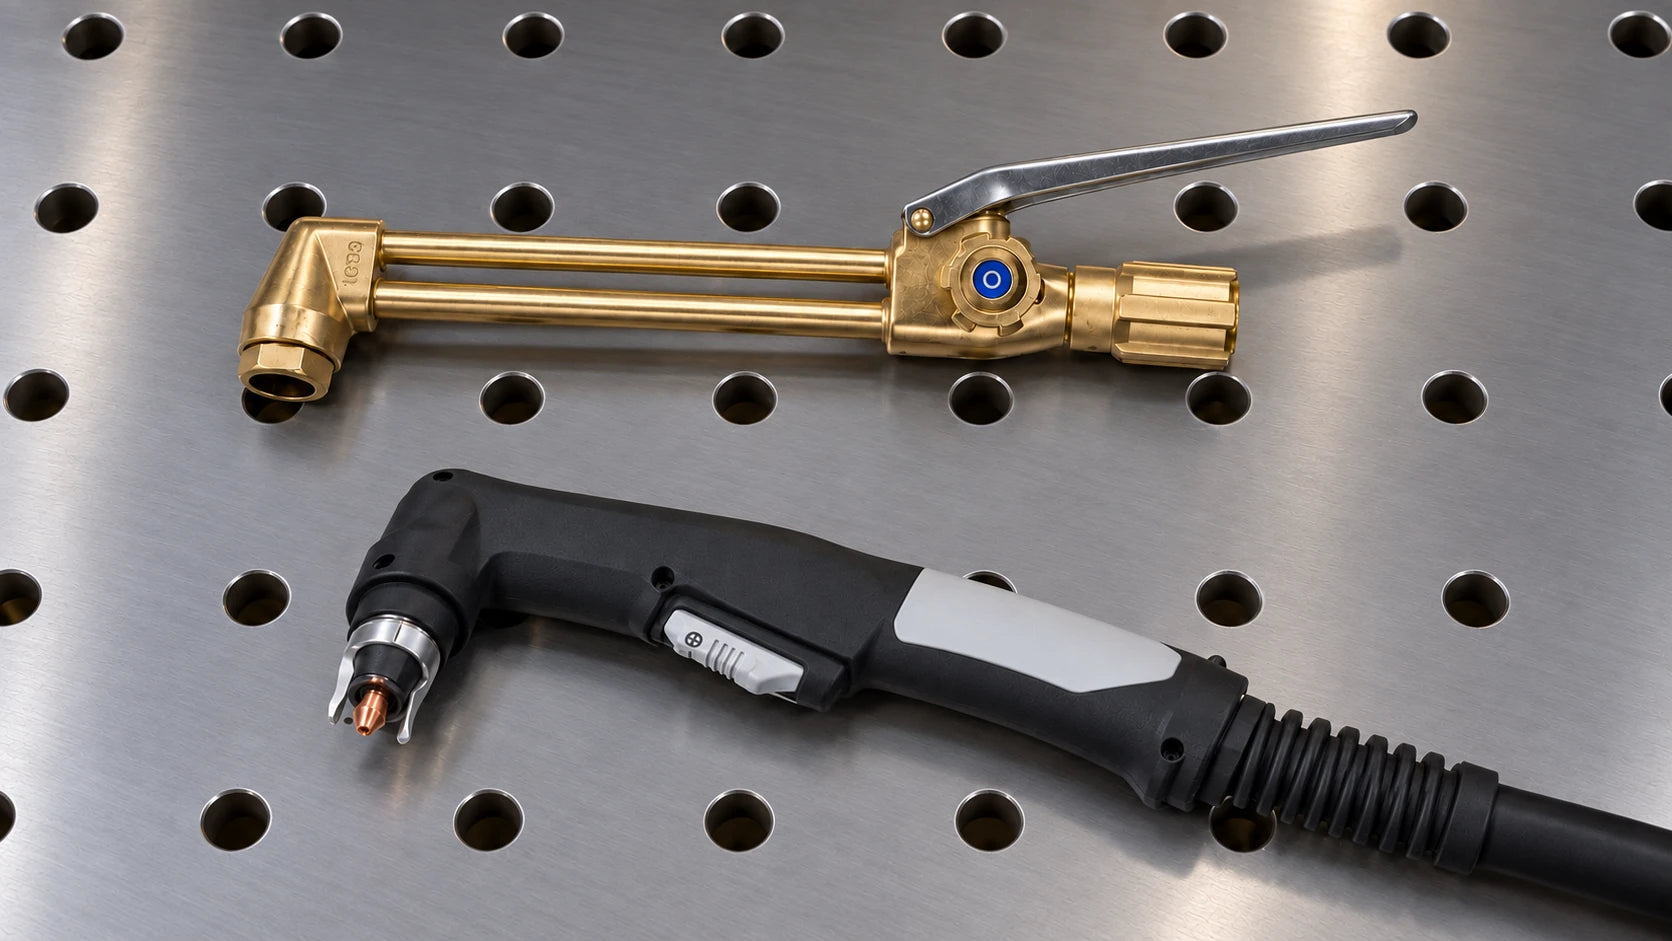
When you think about it, oxy-acetylene cutting and plasma cutting are the same things, right? Or are they?
They both cut through metal, yes, but that’s about where the similarities end. In reality, they’re two totally different processes, and each has its pros and cons.
What is Oxy Acetylene Cutting?
Conventional oxyfuel cutting is mainly used on carbon and low-alloy steels. It is not a general cutting process for every ferrous metal.
Stainless steel, aluminium and many cast irons do not suit ordinary oxyfuel cutting in the same way; specialised methods are separate processes.

What is Plasma Cutting?
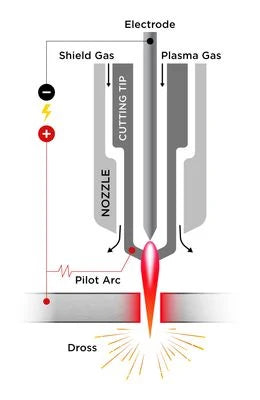
Plasma is a super-heated column of gas. Plasma cutting (plasma arc cutting) is a melting process that uses plasma and an outside power source. It creates an electric arc between the electrode (which is in the torch) and the metal being cut, melting and ejecting it from the cut.
Plasma gas is specific to the system and material. Do not connect hydrogen mixtures or other gases to a cutter designed only for compressed air.
Plasma can cut many electrically conductive materials, but capacity and gas selection depend on the system and material.
Oxy vs Plasma
There are quite a few differences between the two methods, from gas requirements to preheating, travel speed, and portability. So, which is going to work best for you?
PROS
Plasma Cutting
- Plasma cuts electrically conductive materials within the machine's approved range, including many steels and aluminium alloys.
- No preheating
- The air-plasma examples here use compressed air. Industrial plasma systems may use other gases under their own procedures.
- Some machines come with a built-in air compressor (like the Razor Cut 40 Air)
- Stop/start with a single button press
- Less mess and less clean up
- Machines are generally lightweight
- Faster travel speeds, especially on thin materials
- Both processes have significant hazards. Compare the required gas handling, electrical protection, radiation, extraction and fire controls for the actual site.
Oxy Acetylene
- It’s doesn’t need a power source
- Cuts through thick material
- It’s multipurpose – you can weld, gouge, braze, heat and solder, as well as cut
CONS
Plasma Cutting
- Max cut thickness is determined by the machine
- The machine and air compressor require a power source
Oxy Acetylene
- Material range: conventional oxyfuel cutting suits carbon and low-alloy steel; conductivity alone does not determine oxyfuel suitability.
- Metal needs to be preheated before it’s cut
- It requires oxygen and a fuel gas, commonly acetylene. The fuel gas is flammable; oxygen is an oxidiser that supports combustion.
- Longer setup time
- The torch needs to be manually lit and extinguished
- Incredibly messy with lots of clean up
Further Explained…
Plasma Cutting Pros:
- For an air-plasma machine, use the specified clean, dry air supply at the required delivered flow and pressure.
- Plasma doesn’t require any preheating; you can just start cutting your metal as soon as the torch is on.
- Some air-plasma cutters have an integrated compressor; others require an external supply. Both still require their specified electrical supply and controls.
- The torch is ignited and extinguished with the touch of a button instantly, so it’s easier to use, and there’s no need to rotate valves trying to adjust to the gas levels to get the correct flame.
- Dross and edge quality depend on material, consumables, settings and travel speed. Plasma does not always produce an edge requiring no cleanup.
- Compare transport weight for the complete setup, including the compressor where required, rather than treating one older machine's weight as typical.
- You can cut a lot faster with plasma, especially on really thin material, thanks to not needing to preheat.
- Plasma cutting avoids a continuously burning fuel-gas flame, but the arc, hot metal, sparks and electrical supply still create hazards. Release the trigger, make the equipment safe and allow hot components to cool according to the manual before setting the torch aside.
Plasma Cutting Cons:
- Check the exact model and generation for cutting capacity. Similar product names can have different clean-cut and severance ratings.
- The machine and air compressor require a power source (though these days, power points aren’t too hard to find).
Oxy Cutting Pros:
- It doesn’t need a power source, with only a torch and two gas tanks. That means it’s often more favourable if you’re working somewhere remote and there isn’t any access to power.
- Oxyfuel thickness capacity depends on the torch, tip, fuel, oxygen supply and steel condition; use the equipment's cutting chart.
- Heating, brazing and welding require the correct equipment and fuel for that task. A cutting setup is not automatically suitable for fusion welding steel.
Oxy Cutting Cons:
- For ordinary cutting of carbon steel, oxyfuel can be useful at substantial thickness. Do not extend that recommendation to all ferrous alloys.
- The metal needs to be preheated before you can begin cutting, especially on thick sections. The preheating is done with the same torch, but it’s extra time standing and waiting to be ready.
- It requires two gas supplies: oxygen and a fuel, usually acetylene. Both need appropriate storage and handling. Acetylene is flammable; oxygen does not burn but strongly supports combustion.
- Set the gas equipment and preheat flame according to the torch, tip and fuel instructions. Flame adjustment is not identical for every oxyfuel setup.
- Plasma avoids a fuel-gas flame but still presents serious electrical, radiation, fume and fire hazards. Neither process is universally safer.
- Compare the required edge quality and cleanup on a representative sample rather than assuming one process always leaves less dross.
Oxy cutting was the original method of metal cutting, but with new technology, plasma cutting has caught right up, and in a lot of ways, overtaken it.
Choose from the material, thickness, power and gas available, required edge finish and total setup cost.
Sources for revised guidance
Reference diagrams: UNIMIG. Original source attribution is retained.
Related guides
Process guideWhat Is Plasma Cutting? Setup, Consumables and Cut Quality Buying adviceHow to Choose a Plasma Cutter: Capacity, Air Supply and Torches Buying adviceWelding Duty Cycle Explained: Choosing the Right WelderChoose around the cutting job.
Tell us the material, thickness and whether the work is in a workshop or on site.
Ask us about thisTechnical sources and scope
Reviewed 22 September 2026. Manufacturer examples apply to the named equipment; use the current manual for your exact model and the required welding procedure.
- TWI — oxyfuel cutting and material limitations
- Hypertherm — plasma technology and gases
- SafeWork NSW — Welding processes code of practice (2022)
Oxyfuel material limits and process hazards were corrected; capacity remains model- and material-specific.


