
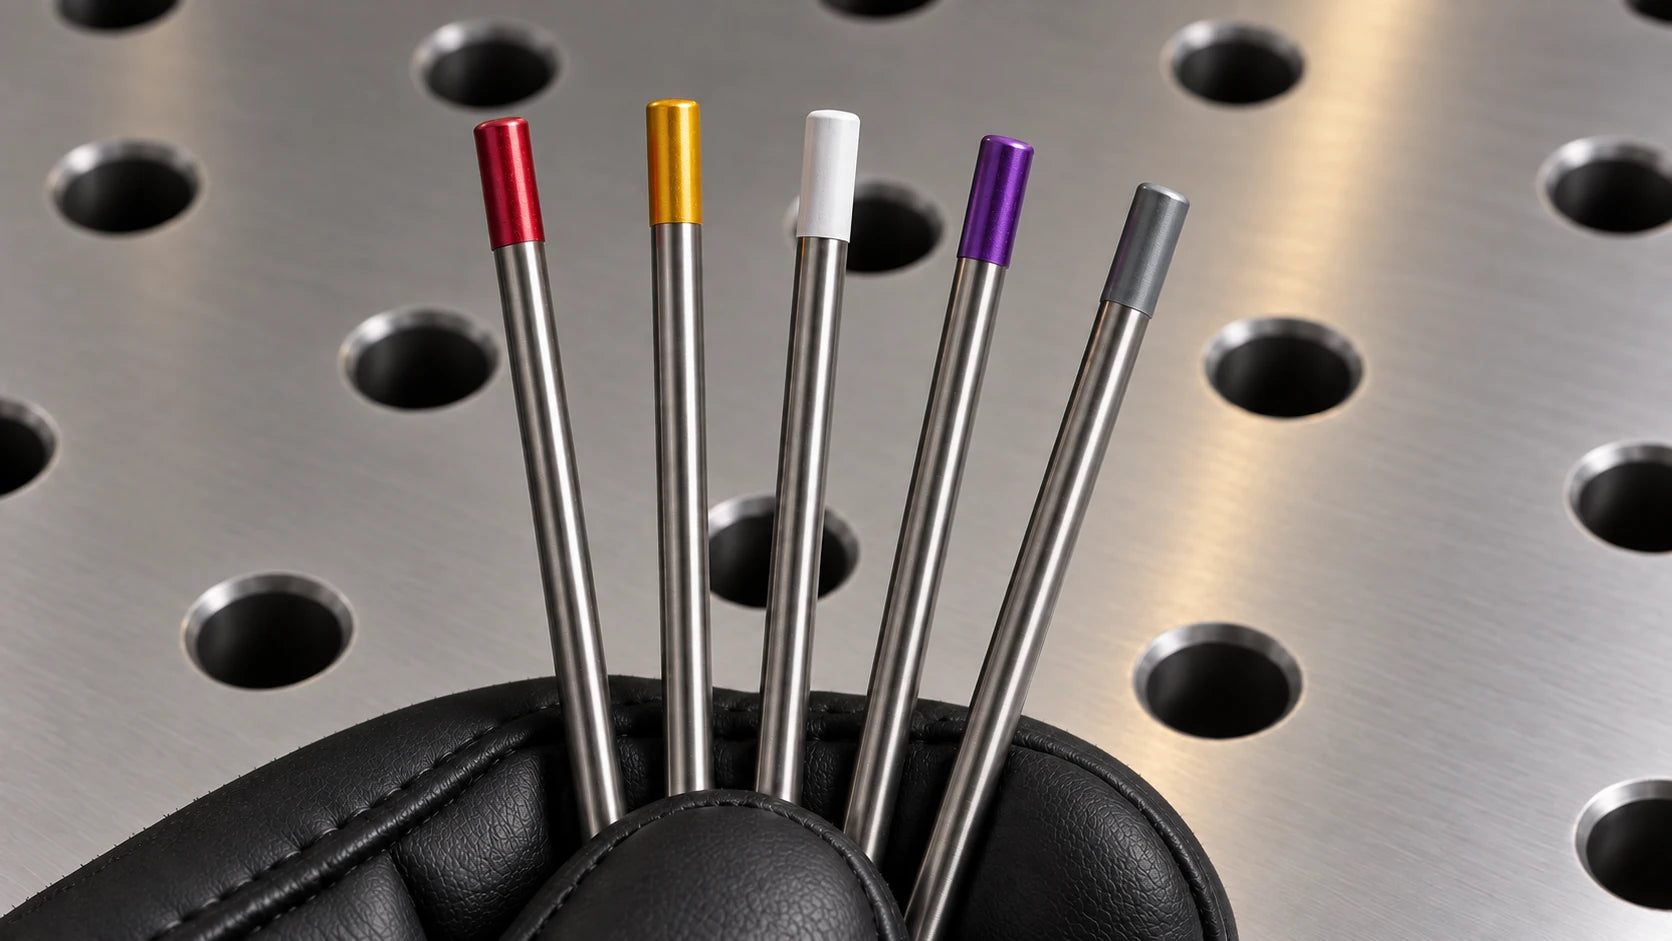
Trying to find the perfect tungsten electrode for the TIG weld you’re planning can seem like a bit of a mission. There are quite a few tungsten types on the market, and every single one of them does something different, even if it’s just slightly.
Identify electrodes by the manufacturer's type marking and data sheet as well as colour. Mixed-oxide products and some colour conventions differ between brands.
What’s in a Tungsten and What Do They Do?
TIG electrodes may be pure tungsten or contain specified oxide additions. Read the actual composition and classification rather than assuming all mixed electrodes behave alike.
Thoriated tungstens were the second type of tungsten that became available, so a lot of the time, they’re used as a reference point when comparing how the other (newer) tungstens perform.
2% Thoriated (red)
2% thoriated electrodes are traditionally used for DC TIG. They are not physically incapable of AC operation, but modern inverter recommendations commonly favour other types.
In technical terms, the added thorium boosts the electron emission qualities in the tungsten. In simple terms, the added thorium means the tungsten needs a lower amount of heat to start and maintain an arc, which has a bunch of benefits:
- Good arc starts
- A very stable arc
- A high current carrying capacity
- Suitable current and tip preparation can limit erosion
- Correct use can reduce electrode contamination; no type is guaranteed never to spit
- It maintains a sharpened point
Thoriated electrodes contain radioactive thorium. Assess handling, grinding dust and disposal using the product safety information and workplace controls.
Do not describe thoriated welding as risk-free. Use an appropriate alternative where suitable, and control dust with dedicated preparation equipment and the required protection.
1.5% Lanthanated (gold)
1.5% lanthanated electrodes can suit AC and DC work. Their current capacity depends on diameter, waveform and polarity; a universal 50% improvement over thoriated electrodes is not supported here.
Note: The current capacity of a tungsten is how many amps it can be run on before it starts to deteriorate.
Lanthanated tungstens also work well on both AC and DC, plus they have:
- One of the best arc starts (especially on DC)
- A very stable arc
- A low burn-off/erosion rate, so they last a long time
- Good re-ignition under suitable settings
- Low erosion when correctly selected and operated
- They can strike and maintain an arc at low or high amperages
- Prepare the tip to suit the power source; a point or truncated point is common on modern inverters
Compare the supplier's operating ranges for the actual electrode size and process.
An oxide addition changes electrode behaviour; it does not make different electrode types electrically identical.
Lanthanated electrodes avoid thorium and are a common general-purpose option, subject to the machine's recommendation.
0.8% Zirconiated ( white )
Zirconiated electrodes are principally intended for AC applications, especially conventional AC. They are not normally the first choice for DC TIG.
- They ball well and retain the shape
- They have an incredibly stable arc
- They can resist contamination under appropriate AC operating conditions
- It handles high amps well (perfect for aluminium)
- Use the published current range for the diameter and AC conditions
They are one AC option; do not assume they are preferable to lanthanated electrodes on every modern inverter.
Rare Earth (purple)
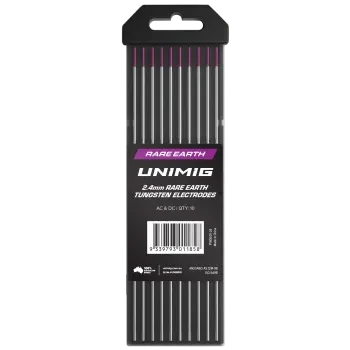
Mixed-oxide electrodes contain a manufacturer-specific blend. Confirm its classification and intended AC/DC applications from the packet and data sheet.
- Great arc starts
- A very stable arc in AC and DC
- Electrode life depends on current, preparation and shielding
- Little spitting
- Choose diameter from the published current range
- Do not undersize an electrode solely because it is sold as rare earth
Purple and chartreuse products are not automatically the same composition. Match the specified product rather than substituting by a general rare-earth label.
2% Ceriated (grey)
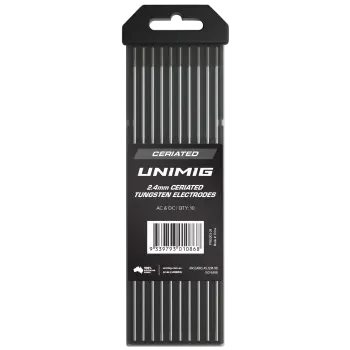
Ceriated electrodes are often useful at lower currents and may be used on AC or DC where the machine and electrode guidance allow.
- Excellent arc starts at low amps
- It runs best on DC with low current settings
- Good re-ignition
- Great arc stability
Because of the way cerium oxides behave when they’re heated to extreme temperatures, it’s not recommended to use them on high amperage applications.
At excessive current the electrode may deteriorate; choose type and diameter within the manufacturer's operating range.
On the flip side, because cerium works so well on low amperages, Ceriated tungstens are perfect for use on sheet metal and thin piping or tubing.
Which Tungsten Do You Need?
| Electrode | Application notes |
|---|---|
| Lanthanated | Common AC/DC option on suitable inverters; identify the actual oxide content and current range. |
| Ceriated | Often useful at lower current; use the maker's AC/DC guidance. |
| Zirconiated | Principally an AC choice; not automatically best for every inverter. |
| Thoriated | Traditionally used for DC; not universally excluded from AC. Thorium requires appropriate handling and dust controls. |
| Mixed oxide / rare earth | Composition varies by product. Colour alone does not establish equivalence. |
Select diameter and tip preparation for current, waveform and polarity. This replaces an unsupported dot-rating chart.
Use the selection notes below with the machine and electrode data sheets. A dot-score comparison is not a standardised performance test.
Arc Ignition
Reliable ignition depends on the power source, settings, electrode preparation and connections.
A weak or difficult start needs diagnosis of the complete setup; brightness or sound alone cannot rank electrode quality.
Tungsten Life
How long does the tungsten last before it needs grinding, or do you need a new one? Tungsten has the highest melting point of any metal on the periodic table, but that doesn’t mean it will last forever.
Every tungsten handles amp rates differently, and the higher the amps, the faster some tungstens lose their tips. There are a few things that will make your tungsten last longer.
Prepare the point, flat or rounded end specified for the power source and application.
Two is being careful not to dip them, which is explained below. Both of these are a great way to make the most out of your tungsten.
Arc Stability
Does the arc flicker or blowout? Is it consistent all the way across the weld? Once the arc has started, it should look like a cone-shaped light that remains totally solid. It shouldn’t flicker, or wander, or blow out if it is stable.
Some things can affect this, like using low amps on thick electrodes, or AC, which is more likely to flicker even when stable, and pulse welding will flick in and out as the arc moves between amp ranges. In general, though, your arc should be steady and maintain that cone appearance for the entire weld.
Resistance to Contamination
How easily does the tungsten become contaminated? One of the main ways that a tungsten becomes contaminated is by dipping it. There are two ways you can dip.
Contact with the workpiece or pool can contaminate the electrode and disturb the arc.
Inspect and reprepare a contaminated electrode before continuing; the amount of contamination varies with the contact.
The second way to dip your tungsten is by touching your filler metal rod directly onto it. Instead of the rod melting into your weld pool, it is now coating the outside of your electrode. This causes instant contamination of your tungsten, and a lot of the time it’ll cause the arc to wander.
Long term constant use of the same tungsten will also naturally build up contaminants, like discolouration from the gas and oxidisation, even if you’re cleaning it regularly.
If you’ve dipped your tungsten into the weld pool, don’t worry, you aren’t the first, and even seasoned welders slip up sometimes. It can be a bit of a pain, as you’ll need to re-grind it into shape before you can continue to use it.
Remove the contaminated end with suitable dedicated cutting equipment, then regrind lengthwise with dust control. Do not snap the electrode; this can split it or leave hidden damage.
Tungstens that are more resistant to contamination will not suffer as much discolouration or have as many contaminants stick to the tungsten if it is dipped and will take longer to ‘dirty’ from extended use.
AC Performance
AC is commonly used for aluminium and magnesium TIG. Specialised DC procedures also exist, so DC is not inherently impossible on those metals.
AC means that the current flows both ways, and a cycle is completed when it has flowed one way and then back the other way. This back and forth of the current has different effects on tungstens than DC (direct current) does, and some tungstens are better suited for AC applications.
Can a thoriated electrode be used on AC?
Some equipment manuals permit it. Suitability depends on the waveform, current, electrode size and preparation.
Follow the actual power-source recommendation. Overheating or tip loss is a reason to stop and correct the setup, not proof that every thoriated electrode fails on AC.
Reference diagrams: UNIMIG. Original source attribution is retained.
Related guides
Process guideWhat Is TIG Welding? Setup, Consumables and Technique Process guideHow to Weld Aluminium: MIG, TIG and Troubleshooting Consumables guideTIG Collet Body vs Gas Lens: Differences and SelectionMatch a tungsten to your TIG setup.
Tell us your machine, material, current range and existing electrode specification.
Ask us about thisTechnical sources and scope
Reviewed 22 September 2026. Manufacturer examples apply to the named equipment; use the current manual for your exact model and the required welding procedure.
- CK Worldwide — tungsten types and classifications
- Miller — electrode preparation and TIG operating manual
- Diamond Ground Products — tungsten preparation guide
- Miller — choosing tungsten for AC TIG
Unsupported electrode rankings, AC exclusions, equivalent-colour assumptions and snapping instructions were removed.


