
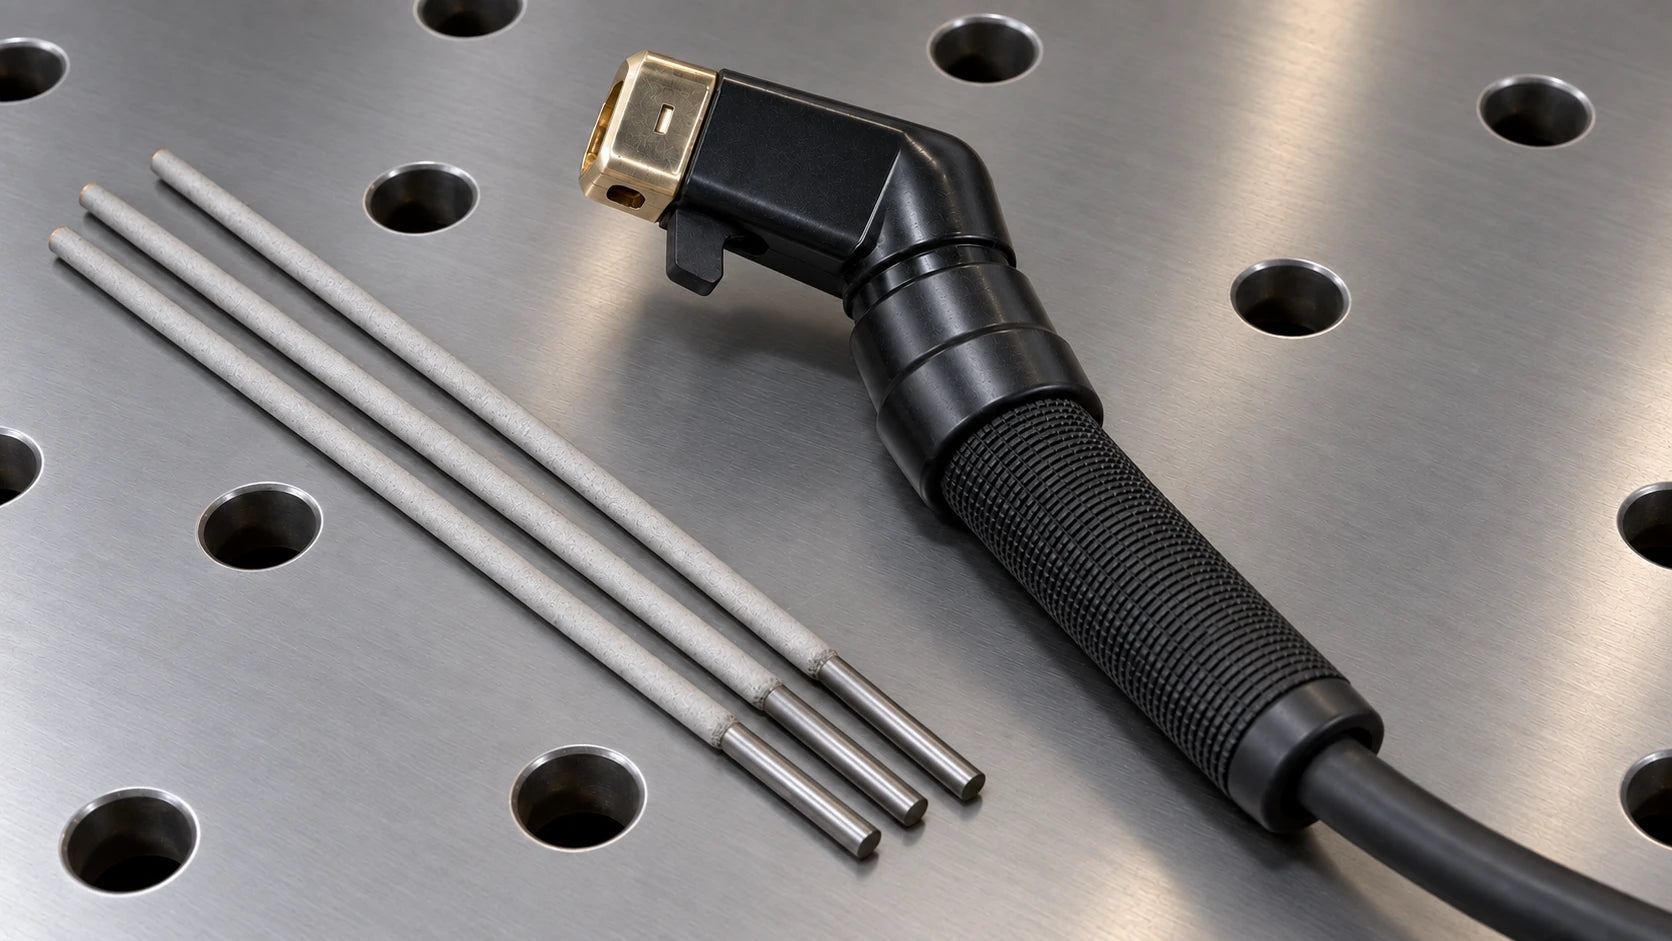
Stick welding is one of the oldest types of welding still used today. It’s simple to set up and relatively easy to learn, which is why a lot of people recommend it for beginner welders.
What is Stick (MMA) Welding?
Manual Metal Arc (MMA) welding is an arc welding process in which an arc is formed between a flux covered electrode and the base metal. The arc melts the electrode into the workpiece, forming the weld.
MMA is also referred to as Shielded Metal Arc Welding (SMAW), but it’s most commonly known as ‘stick’ welding, after the stick like electrodes used for the weld.
How Does Stick Welding Work?
Stick welding is one of the simplest types of welding because it uses the least amount of equipment. It requires a completed electrical circuit to ignite an arc, which is formed by all the components of the welder.
First, an electrode holder is connected to the welder, and the electrode itself is inserted into the holder. An electrode holder is a much simpler ‘torch’ – its only purpose is to hold an electrode in place and allow the welding current to flow through it. There are no buttons or dials involved at all.
The electrode is tapped or struck against the base metal, which ignites the arc between the two. The electrodes used in stick welding are consumable electrodes, as they melt into the base metal to form the weld.
That’s the first half of the electric circuit done.
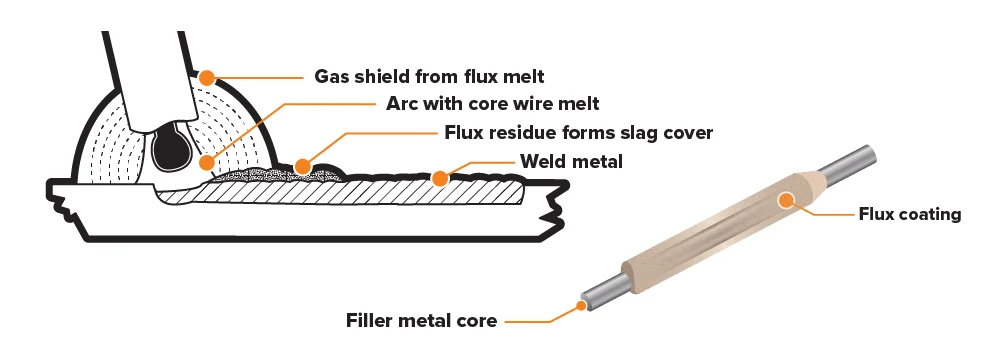
Unlike MIG or TIG, stick welding doesn’t need an external gas. Instead, the outer flux coating on each electrode works to shield the weld as it melts. The flux coating melts with the metal, releasing gases from within which bubble to the surface.
These internal gases protect the weld from outside contaminants until the puddle begins to cool. The flux coating, once melted, forms a layer of slag over the final weld, which needs to be chipped off to achieve a clean, finished weld.
The work-return clamp completes the welding circuit through the workpiece. Attach it to clean metal with a reliable current path; it is distinct from the machine's protective earth.
So, to complete the circuit, make sure you plug your clamp into the machine and connect it to a clean spot on the metal you’re welding.
Stick Electrode Selection
Stick electrodes carry a classification describing their properties. Common AWS carbon-steel examples include E6013 and E7018; other classifications can have additional digits or suffixes.
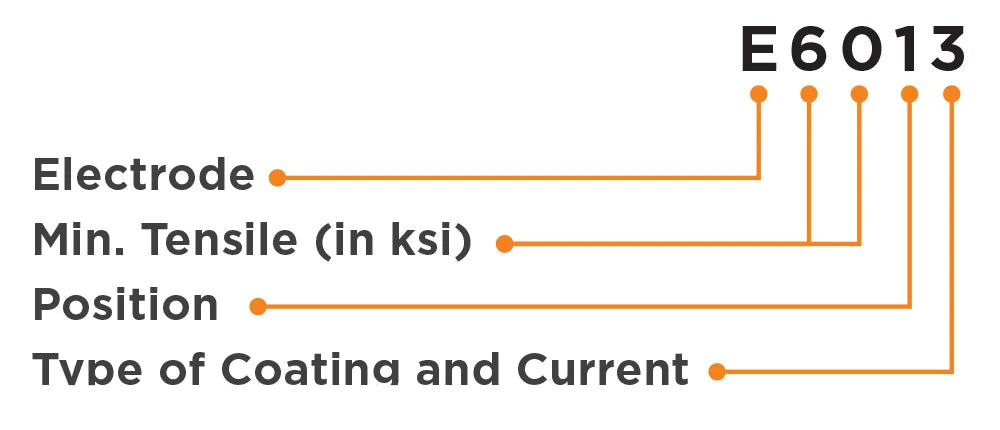
Here’s a breakdown of what each part of the code means:
- In those AWS classifications, E identifies an electrode. Other standards may use different designations.
- For an E6013 electrode, “60” indicates a minimum deposited-weld-metal tensile strength of 60,000 psi (60 ksi). E70-series electrodes indicate 70,000 psi (70 ksi). Select the classification for the base metal, joint and procedure; these values do not cover every metal.
- For common AWS carbon-steel classifications, the first two or three digits identify minimum tensile strength in thousands of psi, depending on the classification.
- The position digit and the final coating/current designation must be read together using the electrode data sheet. The shorthand does not describe every electrode classification system.
Generally speaking, the most common electrodes used for mild steel are E6010, E6011, E6013, E7016, E7018 and E7024. Stainless steel electrodes are marked with their metal grade, e.g., 309L.
E6013 is one general-purpose carbon-steel electrode. Choose the classification for the base metal, required properties, position and available current type.
Select electrode diameter and current from the electrode manufacturer's range and joint procedure, not material thickness alone.
Settings
Current is a key setting, but polarity, output type, arc-start behaviour and electrode compatibility also matter.
What you want to set your amps to depends on a couple of things, including the electrode type and diameter, the base metal thickness, and your weld position.
Most electrode packets will come with a recommended range of amps that the electrode can handle/will melt at, so even if you’ve got no idea, they provide a good starting place. Starting in the middle of the recommended range and adjusting up or down as needed is usually the best way to find what’s going to work for you.
Polarity
Stick welding can be done in AC or DC.
On DC, connect the electrode holder and work return for the polarity specified on the electrode data sheet.
DCEP means the electrode is positive; DCEN means it is negative.
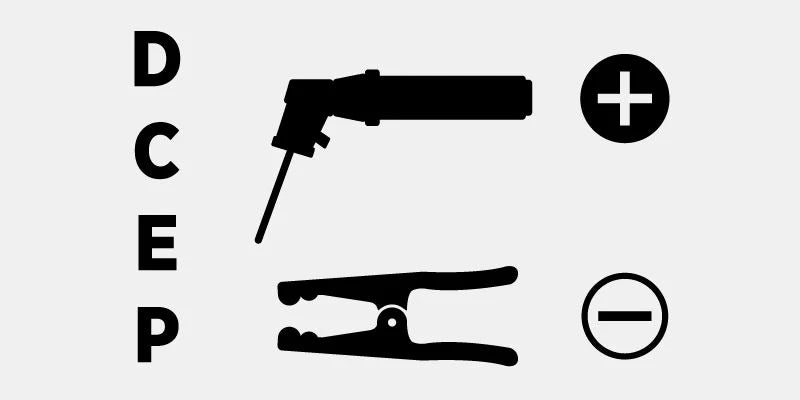
Changing polarity affects electrode behaviour, but the effect on penetration depends on the electrode and procedure.
Do not choose polarity from a universal deeper-versus-shallower rule.
Each stick electrode will say whether they should be used in DCEP, DCEN or AC on their packaging.
To set up a UNIMIG welder for DCEP, plug the electrode holder cable into the positive (+) panel mount and the earth clamp into the negative (-) panel mount.
For DCEN, plug the electrode holder cable into the negative (-) panel mount and the earth clamp into the positive (+) panel mount.
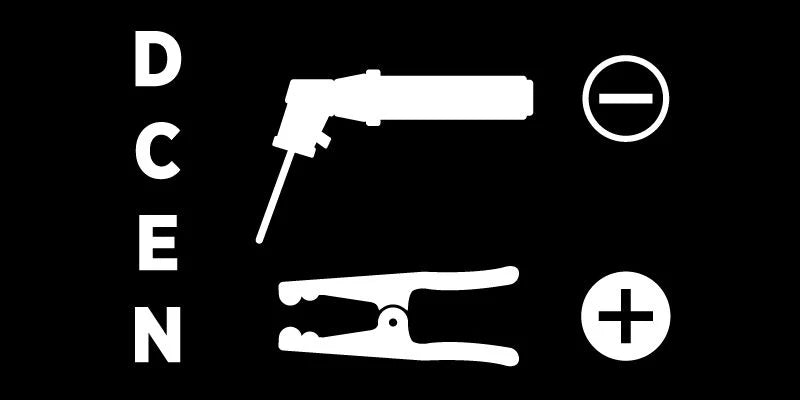
AC stick welding requires a machine with an AC stick mode. AC TIG capability alone does not guarantee that feature.
AC stick welding requires a power source with an AC stick output mode and an electrode approved for AC. An AC-rated electrode does not turn a DC output into AC. Follow the machine manual for its output mode and lead connections.
Metals
Common stick-welding materials include:
- Mild steel
- Stainless steel
- Cast iron
Common Stick Applications and Fabrications
Other alloys can also be welded with specialised electrodes and procedures. The common examples above are not a complete material list.
Some common stick welding uses include:
- Construction – stick is used for suitable structural joints under the required welding procedure and qualification.
- On-site and outdoor work – because it’s gas free (and stick dedicated machines are relatively small), it’s the first pick for outdoor work and on-site work thanks to its portability.
- Fabrication and repairs – a practical option for many steel frames and repair jobs; thin sheet takes more control and may suit another process better.
- Pipe work – stick is one option among several processes; select it through the pipe material, joint and service requirements.
- Home hobby use and DIY projects – the simple setup and lower costs make stick welding a great choice for weekend warriors, plus they’re small, so they’re easy to store.
- Mining – portable equipment may be useful, but site electrical and welding controls still apply.
- Underwater – specialist commercial-diving work can use wet or dry welding and more than one process. It is not an application for ordinary workshop equipment or untrained operators.
Advantages of Stick
There are plenty of reasons why stick is still so popular in the welding industry and why it won’t be going anywhere.
- A compact stick welder can be portable, but the location still needs suitable electrical, fire, fume and weather controls.
- It’s easy to learn. The hardest part of stick welding is consistently striking an arc, the rest of the process is super simple, and it’s great as a starting point for welding.
- Without an external shielding-gas supply, stick is less sensitive to draughts than gas-shielded processes. It is not suitable for unrestricted use in wind, rain or wet conditions.
- Remove contamination and prepare the joint as required. An electrode's tolerance of some surface condition is not permission to weld over unknown coatings or heavy rust.
- A basic stick setup can be economical. Include suitable leads, holder, work-return clamp, electrodes, PPE and fume controls in the cost.
- Thick joints can be built with multiple passes using a suitable preparation and procedure. Amperage alone cannot compare the thickness capability of stick and TIG.
Disadvantages of Stick
While it has its advantages, there are still a few reasons you wouldn’t pick stick.
- It’s slow. The travel speed with a stick electrode, paired with the need to grab a new one each time it runs out, adds up, making it a time-consuming way to weld.
- It’s messy. Stick welding produces a lot of spatter and smoke, much more than TIG or MIG does. Plus, some electrodes are more aggressive, creating more spatter.
- There’s extra downtime. Once you’re done with the weld, you’ve still got a bit of extra work before the job is done removing slag from each weld. Depending on the electrode you’re using, this can be easy, or it can be a bit of a challenge.
- Electrode choice, thin-material control and post-weld slag removal can limit suitability for some jobs.
- Thin material is challenging because of burn-through risk, but there is no universal 2 mm lower limit. Do not change to DCEN unless the electrode and procedure permit it.
If you want to get into welding, stick welding is a great, cost-effective way to learn how to weld, and it’s a skill that can be used across a range of applications.
Sources for revised guidance
Reference diagrams: UNIMIG. Original source attribution is retained.
Related guides
Process guideStick Welding Guide: Electrodes, Setup and Technique Process guideWhat Is MIG Welding? Setup, Wire Feed and Technique Buying adviceBest Beginner Welder Australia 2026: MIG, TIG or Multi-Process?Put together a suitable stick setup.
Tell us your machine, material and the type of work you intend to do.
Ask us about thisTechnical sources and scope
Reviewed 22 September 2026. Manufacturer examples apply to the named equipment; use the current manual for your exact model and the required welding procedure.
- Miller — selecting stick electrodes
- Miller — stick technique, arc length and travel angle
- TWI — wet and dry underwater welding processes
- SafeWork NSW — Welding processes code of practice (2022)
Electrode classification, polarity and process limits were corrected, including specialist underwater work.


