
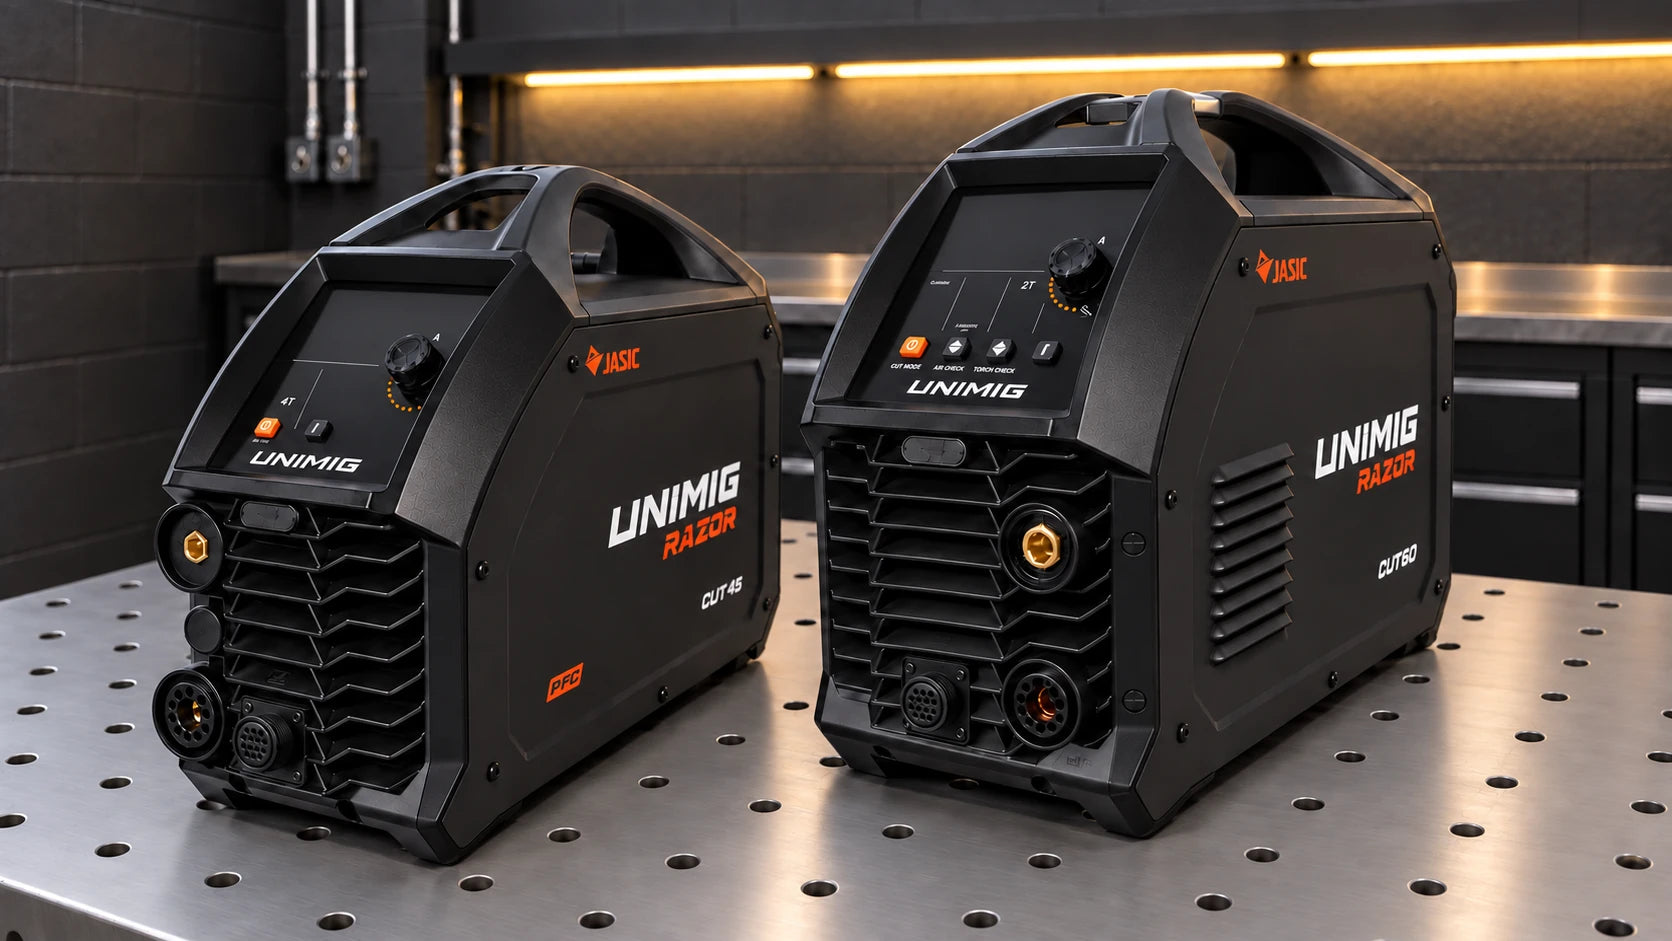
Plasma cutting is a melting process that uses plasma and an outside power source to create an electric arc between the electrode and the metal being cut. The plasma jet melts the metal to make the cut, and the air attached to your machine blows it away. Plasma can cut through anything electrically conductive; steel, stainless steel and aluminium are all fair game.
So, what do you need to get to get started with your plasma cutting?
Air Compressors
The air-plasma cutters discussed here require the specified compressed-air supply, either external or built in. This is not a rule for all plasma technology: some systems use other gases.
Match the compressor’s delivered flow at the required operating pressure to the plasma cutter’s inlet requirements, with capacity for sustained cutting. Do not compare an intake/displacement figure directly with the cutter’s delivered-air requirement. Check the exact manual for pressure, flow and air quality.
Your plasma cutter will state the litres per minute (L/min) it uses, so you’ll want a compressor that states a higher number than that. You don’t want to run out of air before you’ve finished your cut.
You can also buy plasma cutters that have a built-in air compressor. There are benefits to both options, so you’ll need to consider before deciding which will work best for you.
| Pros | Cons | |
| External Air Compressor | Separate compressor can be sized for sustained flow | Extra equipment, hose and power requirements |
| Built-in Air Compressor | One integrated unit to transport | Check the integrated compressor's capacity and duty limits |
Clean Cut vs Severance
You can get two types of cuts with your plasma cutter: a clean-cut or a severance cut.
Clean cut: a smooth, clean-cut through the metal.
Severance: a cut all the way through, but it won’t be smooth or pretty, and if you plan on working on it after, you’ll need to clean it up.
Manufacturers may quote several cutting ratings with different quality and speed criteria. Compare the same material and rating type; severance is not a production-quality recommendation.
Pilot arc and arc starting
Pilot arc describes an arc established in the torch before transfer to the work. HF and contact/blowback starting are ways a system may initiate that arc.
An HF-start system uses high-frequency energy during ignition. It does not inherently require the torch to touch the work or guarantee shorter consumable life.
Contact or blowback designs use an internal starting mechanism without HF. Follow the system's instructions; pilot-arc capability is not a reason to ignore surface condition or coating hazards.
HF can interfere with nearby equipment. CNC compatibility depends on the whole installation, including its interface and electromagnetic controls, rather than a rule that every CNC torch must use one start type.
Confirm the start method and compatible torch for the exact UNIMIG model and generation.
Plasma Cutters
VIPER CUT 30 Mk II Plasma Cutter
- Comes with an SC30 Plasma Torch
- CNC connection
- Pilot Arc start
- 12mm Clean Cut
- 14mm Severance
- Duty cycle: confirm the exact model's output and test-temperature rating
- Air supply: confirm delivered flow and operating pressure in the U14005K manual
- 10 AMP plug
The VIPER CUT 30 Mk II U14005K is a compact 10 A example with an SC30 torch and CNC connection. Its advertised mild-steel ratings are 12 mm clean cut and 14 mm severance. Confirm circuit suitability and the complete CNC requirements; no machine suits every use case.
View more info: VIPER CUT 30
RAZOR CUT 40 AIR Plasma Cutter
- Comes with an SC80 Plasma Torch
- Built-in air compressor
- Pilot Arc start
- Clean cut: confirm the rating for the selected internal or external air mode
- Severance: confirm the exact model documentation; reviewed supplier figures conflict
- Duty cycle: 25% @ 40A
- Air supply: confirm requirements separately for internal and external compressor operation
- 15 AMP plug
The discontinued RAZOR CUT 40 AIR U14001K includes a compressor and also supports external air. Its published cutting figures vary between documents, so ask for the serial/model-specific rating before buying or choosing a cut. Its listed supply is 240 V single-phase with a 15 A plug.
View more info: RAZOR CUT 40 AIR
The original photograph is no longer available. The named equipment and surrounding information have been retained.
RAZOR CUT 45 Plasma Cutter
- Comes with an SC80 Plasma Torch
- CNC connection
- Pilot Arc start
- 16mm Clean Cut
- 20mm Severance
- Duty cycle: 25% at 45 A, at 40°C (KUPJRRW45 manual)
- Gas flow: 189L/min
- 15 AMP plug
View more info: RAZOR CUT 45

RAZOR CUT 80 Plasma Cutter
- Comes with an SC80 Plasma Torch
- CNC connection
- Pilot Arc start
- 30mm Clean Cut
- 35mm Severance
- Duty cycle: 40% at 80 A, at 40°C (KUPJRRW80 manual)
- Air supply: 189 L/min at the specified operating pressure (KUPJRRW80 manual)
View more info: RAZOR CUT 80
The original photograph is no longer available. The named equipment and surrounding information have been retained.
RAZOR CUT 120 Plasma Cutter
- Comes with an SC120 Plasma Torch
- CNC connection
- Pilot Arc start
- 45mm Clean Cut
- 60mm Severance
- Duty cycle: 60% at 120 A and 100% at 100 A, at 40°C (U14002K manual)
- Air supply: manufacturer document sections give inconsistent flow figures; obtain written confirmation for this model before sizing the compressor
View more info: RAZOR CUT 120
These are model-specific examples, including discontinued generations. Check supply phase and circuit, cooling, air demand, duty cycle and CNC compatibility individually. A 15 A plug does not guarantee an existing home circuit is suitable.
Plasma Torches
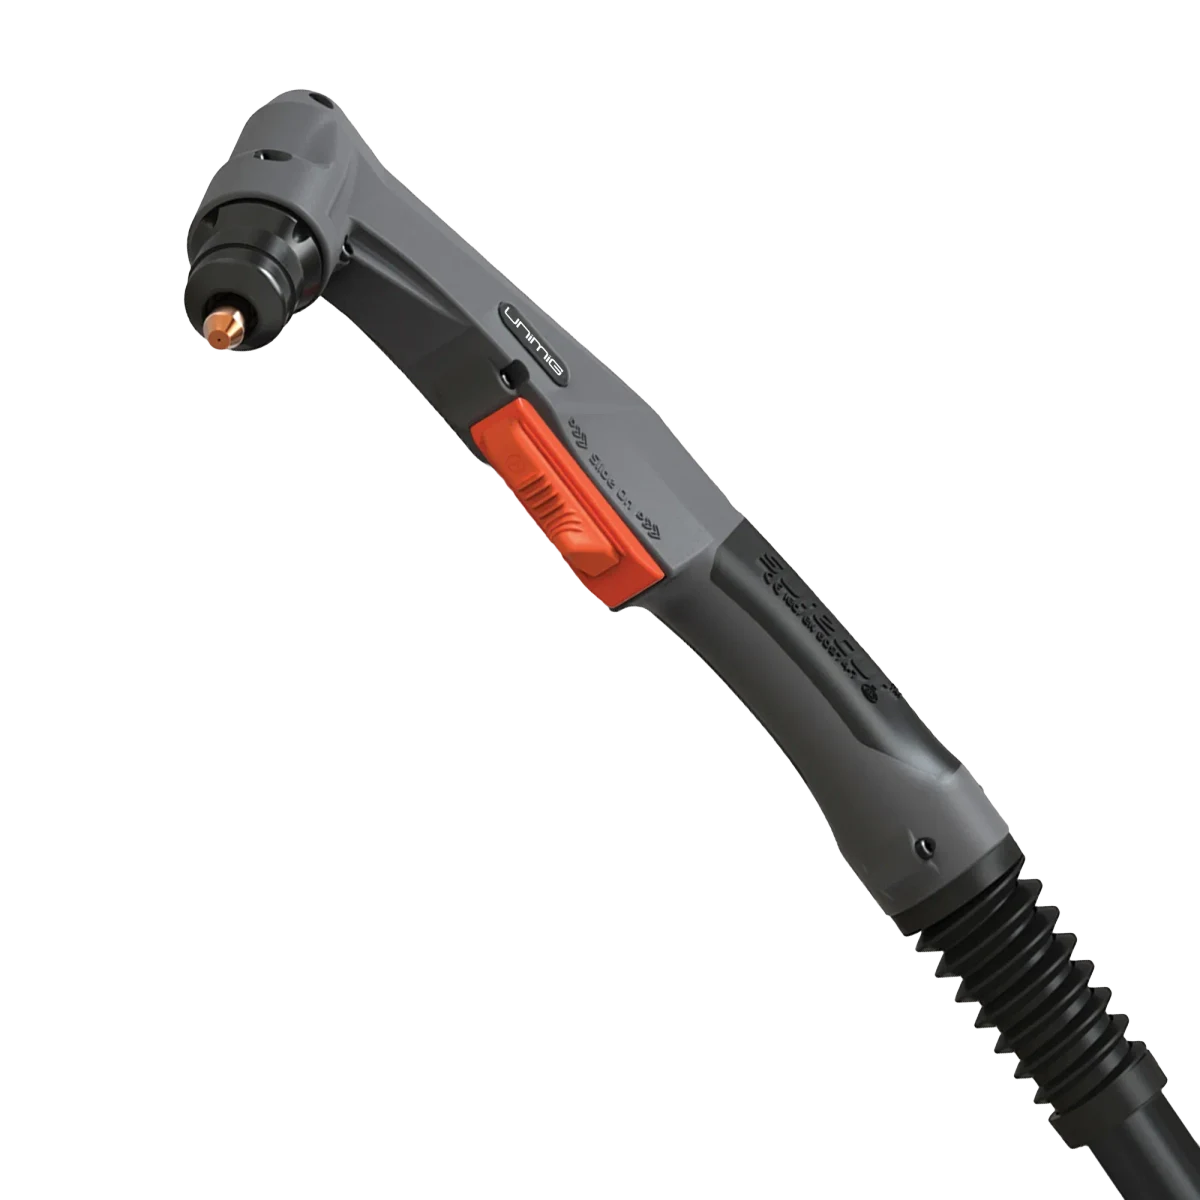
SC30 Plasma Torch
- Stand off cutting
View more info: SC30 Plasma Torch

SC80 Plasma Torch
- Contact cutting
- Stand off cutting
- Gouging
View more info: SC80 Plasma Torch
Use only a torch and consumables approved for the power source. Matching pins does not make an HF torch interchangeable with a blowback system. Drag, stand-off and gouging need their specified consumable sets.

SCM80R Plasma Torch
- Duty cycle: check the exact SCM80R torch data sheet and operating conditions
- Pilot Arc
The SCM80R is a mechanised-torch example. Confirm compatibility with the power source, CNC interface and height-control system, and check current availability with the supplier.
View more info: SCM80R Plasma Torch
Sources for revised guidance
Reference diagrams: UNIMIG. Original source attribution is retained.
Related guides
Process guideWhat Is Plasma Cutting? Setup, Consumables and Cut Quality Comparison guideOxy-Acetylene vs Plasma Cutting: Which Process Fits the Job? Buying adviceWelding Duty Cycle Explained: Choosing the Right WelderChoose a cutter for your everyday material.
Tell us what you cut, its usual thickness and the power and air available.
Ask us about thisTechnical sources and scope
Reviewed 22 September 2026. Manufacturer examples apply to the named equipment; use the current manual for your exact model and the required welding procedure.
- Hypertherm — plasma technology and gases
- Hypertherm — Powermax45 SYNC air supply requirements
- UNIMIG — legacy KUPJRRW45 information sheet
- UNIMIG — legacy CUT 40 AIR U14001K information sheet
- UNIMIG — KUPJRRW80 operating manual
- UNIMIG — CUT 120 manual (conflicting air-flow entries; confirmation required)
- UNIMIG — VIPER CUT 30 Mk II U14005K
- UNIMIG — discontinued model support catalogue
Conflicting CUT 40 AIR capacities and CUT 120 air-flow entries require written manufacturer clarification. Disputed values are withheld; older model generations are separated from current buying advice.


